Induction Heat Treating, Tempering, & Hardening
A Guide to the Heat Treating Process
Some of our customers send their products to outside heat-treaters for induction heat treating (hardening and tempering). The heat treater then sends back the heat-treated parts and the manufacturing cycle continues. However, some customers are starting to bring their heat treating back in-house, while others are seriously considering it. Why?
- The manufacturer wants to have tighter control over their intellectual property and trade secrets. Often, a manufacturer will be reluctant to allow the recipe for their “secret sauce” to leave their plant and their immediate control.
- The manufacturer wants to have tighter quality control. Many have experienced parts getting damaged during shipment to or from the heat treater.
- The manufacturer wants to control costs. Outsourcers often increase prices year after year, and shipping costs continue to increase.
- The manufacturer wants to switch from expensive oven heat treating furnaces to energy-efficient, cost-effective induction heating.
Considering bringing your induction heat treating back in-house but need to know more? We can help.
Industries That Rely on Induction Heat Treating
We supply induction heat-treating and hardening equipment to manufacturers across industries, including:
- Aerospace: landing gear and structural steel components
- Automotive: gears, shafts, and axles requiring wear-resistant surfaces
- Fastener Manufacturing: high-strength bolts and fasteners
- Oil & Gas: drill components and pipeline hardware
- Military & Defense: mission-critical steel parts
Induction Hardening
What is Hardening?
Hardening increases the strength of steel. The process usually involves a heat treatment in which a “hard” microstructure known as martensite is produced.
In conventional hardening processes, steel is heated to a predetermined target temperature, held at that temperature for a fixed amount of time, and then rapidly quenched (cooled down with water) to room temperature or lower. Steel can also be air cooled (“normalizing”), but this method is much slower than quenching.
Induction Zone Hardening
The beauty of induction heating is that you can localize the heat by positioning the induction coil right at the part of the workpiece, or zone, that you wish to heat treat without affecting the rest of the workpiece area.
This zone-specific approach gives precise control over case depth and hardness pattern, ideal for parts that only need a hardened surface in specific high-stress areas rather than a full through-hardening. For more on targeting specific zones and materials, read our guide to Selective Heat Treatment Using Localized Induction Heating.
Induction Scanning
Depending on the length of a workpiece, you can either heat treat the entire length of the workpiece or, if the workpiece length is too long, it is far more economical to “scan” the part. That means you heat treat the part one section at a time until the entire length is heat-treated.
In the photo shown, the induction coil is used to heat only one section of the metal piece. For longer workpieces, you can either move the piece through the coil or move the coil along the workpiece, usually via automation.
For more information about heat treating workable length, contact our heating experts.
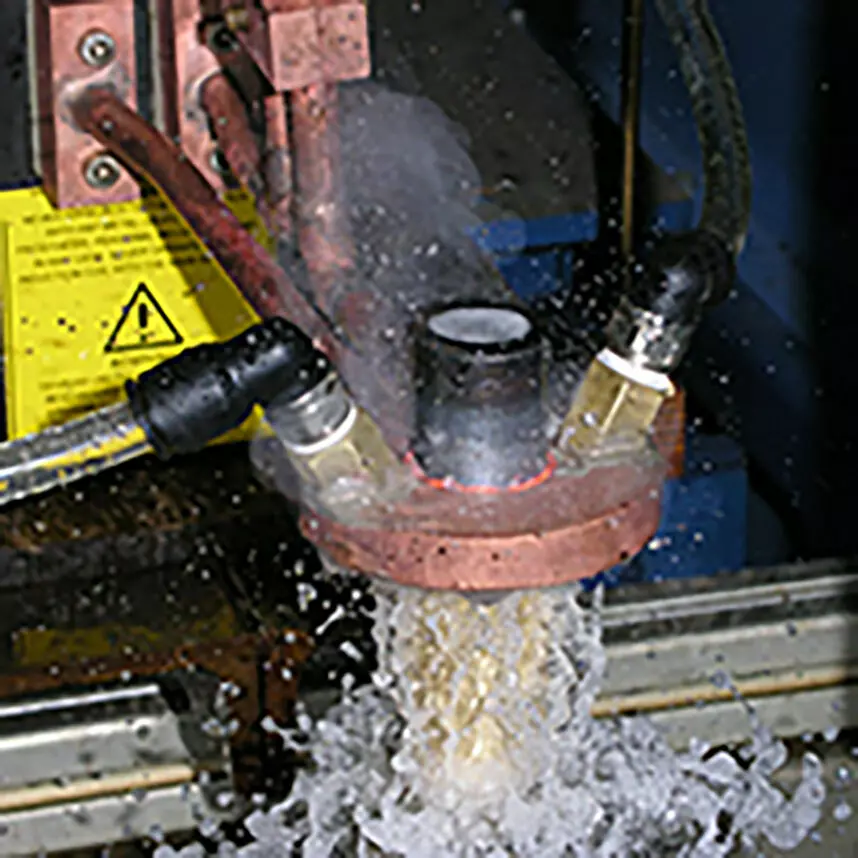
Induction Heat Treating, Heat & Quench
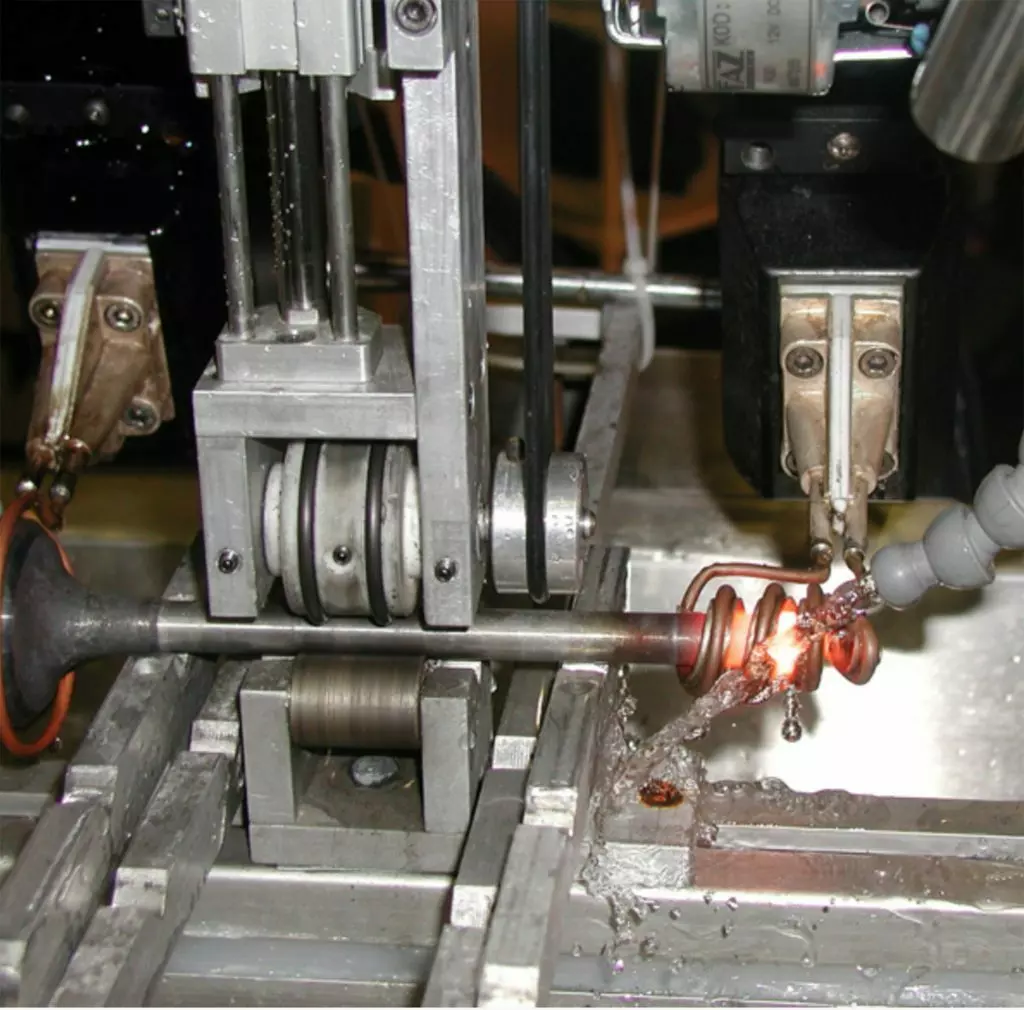
Induction Heat-Treating Scanning Method
Induction Tempering
While hardened steel is very strong, uneven cooling can cause microscopic stresses. Reheating the steel, known as “Tempering”, can correct these micro stresses and result in a more durable material. While the hardness of the material is reduced somewhat, the material is more durable as it is less brittle.
The same induction machine and coil can be used for tempering your workpieces as for hardening. All it requires is adjusting the power supply to generate less heat. Because the same equipment handles both steps, many manufacturers automate the transition between hardening and tempering to keep high-volume production consistent. See how this works in our guide to Induction Heat Treating and Automation.
How Do I Know I’m Heating My Metal to the Right Temperature?
The most effective way is to use an infrared (IR) temperature sensor, or pyrometer. IR sensors can coordinate with and control the induction power supply, cutting power automatically when the workpiece has reached the desired temperature. There are many different choices of IR sensors, so contact our team to find the most reasonably priced, effective sensors for your application.
Automating the Induction Hardening Process
Our high performance induction power supplies work great with automated equipment! Opportunities for automation include:
- Feeding
- Loading and Unloading
- Scanning
- Quenching
- Any other point in the process where manual handling is necessary
Reach out to our heating experts so we can review your particular requirements and determine the best solution. For real-world examples of automated hardening and tempering lines, see our full breakdown in Induction Heat Treating and Automation.
Induction Power Supply Selection
Not all induction power supplies are the same. Many may heat metal well, but when the metal temperature rises above the Curie point, i.e., the metal is no longer magnetic, its resistivity will change abruptly, and the power supply will begin to struggle.
With our high-performance induction power supplies, the induction heater adjusts its output to adapt to the metal’s ever-changing Resistivity and Curie point.
Equipment for In-House Induction Heat Treating
Bringing heat treating in-house typically requires:
- Induction power supply sized to your part and throughput
- A custom-designed induction coil matched to your part geometry and hardening zone
- An IR temperature sensor/pyrometer for accurate, repeatable temperature control
- A chiller to cool the generator and coil during continuous production
- Automation for feeding, scanning, and quenching in high-volume operations

Ready to Bring Your Heat Treating In-House?
Whether you're evaluating induction hardening and tempering for the first time or ready to spec out equipment, our team can help you determine the right power supply, coil design, and automation setup for your parts. Request a Quote or Request a Demo to see induction heat treating in action.
Try our free calculator
Check out our Induction Heating Calculator for running basic calculations to help you size your induction heating applications.
FAQs
1. What is induction heat treating?
Induction heat treating uses electromagnetic energy to rapidly heat steel components for hardening or tempering, without an open flame or oven. A coil positioned around or near the workpiece generates heat, then the part is quenched to harden it, or gently reheated to temper it, improving strength, durability, and wear resistance.
2. What's the difference between induction hardening and case hardening?
Case hardening is a general category of processes, like carburizing or nitriding, that harden only a component's outer surface while keeping the core softer and tougher. Induction hardening is one method of producing a hardened case: it uses electromagnetic heating and rapid quenching to harden a precise zone or depth, often faster and cleaner than furnace-based methods.
3. What metals can be induction hardened?
Induction hardening works best on ferrous metals such as carbon and alloy steels that contain enough carbon to form martensite when quenched. Because the process relies on a metal's magnetic properties, it becomes less efficient above a material's Curie point, and non-magnetic metals like aluminum, copper, or brass typically can't be induction hardened this way.
4. How deep does induction hardening penetrate?
Case depth in induction hardening depends on the coil design, frequency, and power applied, and can range from a thin surface layer to a through-hardened section. Zone or scan hardening lets manufacturers target only the areas that need wear resistance, precisely controlling hardness depth without affecting the rest of the part.
5. Can induction heat treating be automated?
Yes. Induction power supplies pair easily with automated feeding, loading, scanning, and quenching equipment, allowing manufacturers to run consistent, high-volume hardening and tempering cycles with minimal manual handling. This makes induction a practical option for facilities bringing heat treating in-house and scaling production without adding oven-based infrastructure.
Why choose induction technology solutions?
Free Application Testing & Demos Available
Large In-Stock Inventory for Fast Lead Times
Lower Cost & Increase Productivity with Automation
Personable Customer Service
Our experts are ready to help!
Call one of our Engineering Information Specialists